After exception registration, there is no person in charge, and the problem is easy to stay on the bulletin board. Allowing only registrants to close may slow down processing. The MES exception process should separate on-site control, cause analysis and processing confirmation, so that each step has clear actions and responsibility positions.
The warehouse has issued materials, the process has started and the final process has been completed, describing different stages respectively. Directly subtract these records to obtain the quantity in production, which will jump when encountering supplementary recording and cancellation. The Kanban board must explain the statistical scope, deadline and business events on which it is based.
Equipment stopping can only indicate status changes, but cannot automatically explain the reasons. Reason: Too many options will increase the burden of filling in, and too few options will not support improvement. Outage classification should start from the facts that can be judged on site, and collect the information required for subsequent analysis in layers.
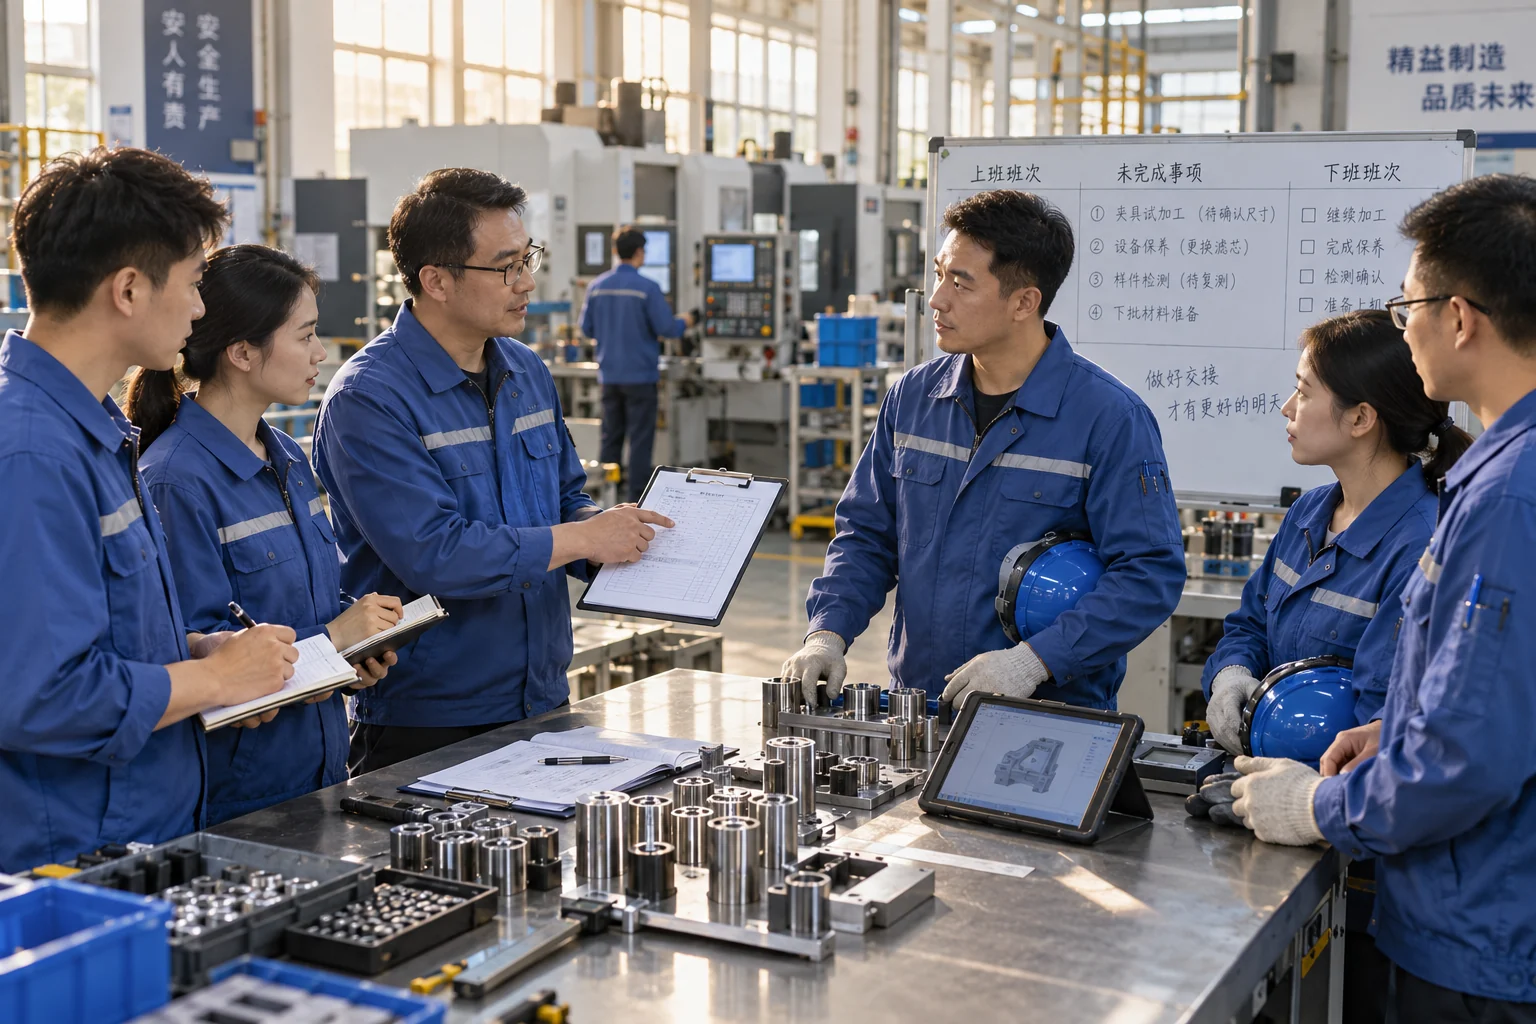
End of shift does not mean end of work order. Unhandled alarms, semi-finished products waiting for inspection, and remaining materials will all affect the next shift. Only a paragraph of handover notes is left, and the successor still needs to ask each item one by one. The system can organize these contents into a to-be-confirmed list.
The function of first article inspection is to confirm whether the current preparation conditions can enter normal production. If the inspection form is only filled in afterwards and a large number of work orders have been reported, the system will lose process constraints. It is necessary to set inspection nodes according to the actual process and clarify the task status when it fails.
One raw material batch may supply multiple work orders, and one work order may also use multiple batches. Just filling in a raw material number on the finished product makes it difficult to answer the question where the batch flows. Traceability should record inputs and outputs as relationships, not just text fields in finished product files.
Device collection is not always online continuously. After the network is interrupted, only saving the last state will lose the production process; re-uploading indiscriminately after the connection is restored may cause repeated counting. The collection end and the server end need to jointly define the supplementary transmission rules.
The output mentioned on site may refer to the quantity completed by processing, or it may refer to the quantity passed through inspection. If different teams each fill in a number, it will be easy to double-count reworked parts when summarizing. MES reporting needs to first explain the business meaning of the quantity, and then decide how to count the Kanban.
After the product process is changed, the parameters used at that time should still be able to be found in historical work orders. Directly covering the process table will make the process records of old batches apply new standards, making subsequent reviews difficult to interpret. There should be a clear relationship between the process version and the work order, and the effective scope of the version also needs to be recorded separately.
Temporarily added orders often cause the originally scheduled tasks to be moved back as a whole. If the scheduling page only allows work orders to be dragged, what you see on site is the new sequence, but you don’t know whether the materials are available, whether the equipment can be processed, or which customers’ delivery dates will be affected. When handling urgent orders, the plan before adjustment should be retained, and it should be clear who proposed the change and why.

 中文